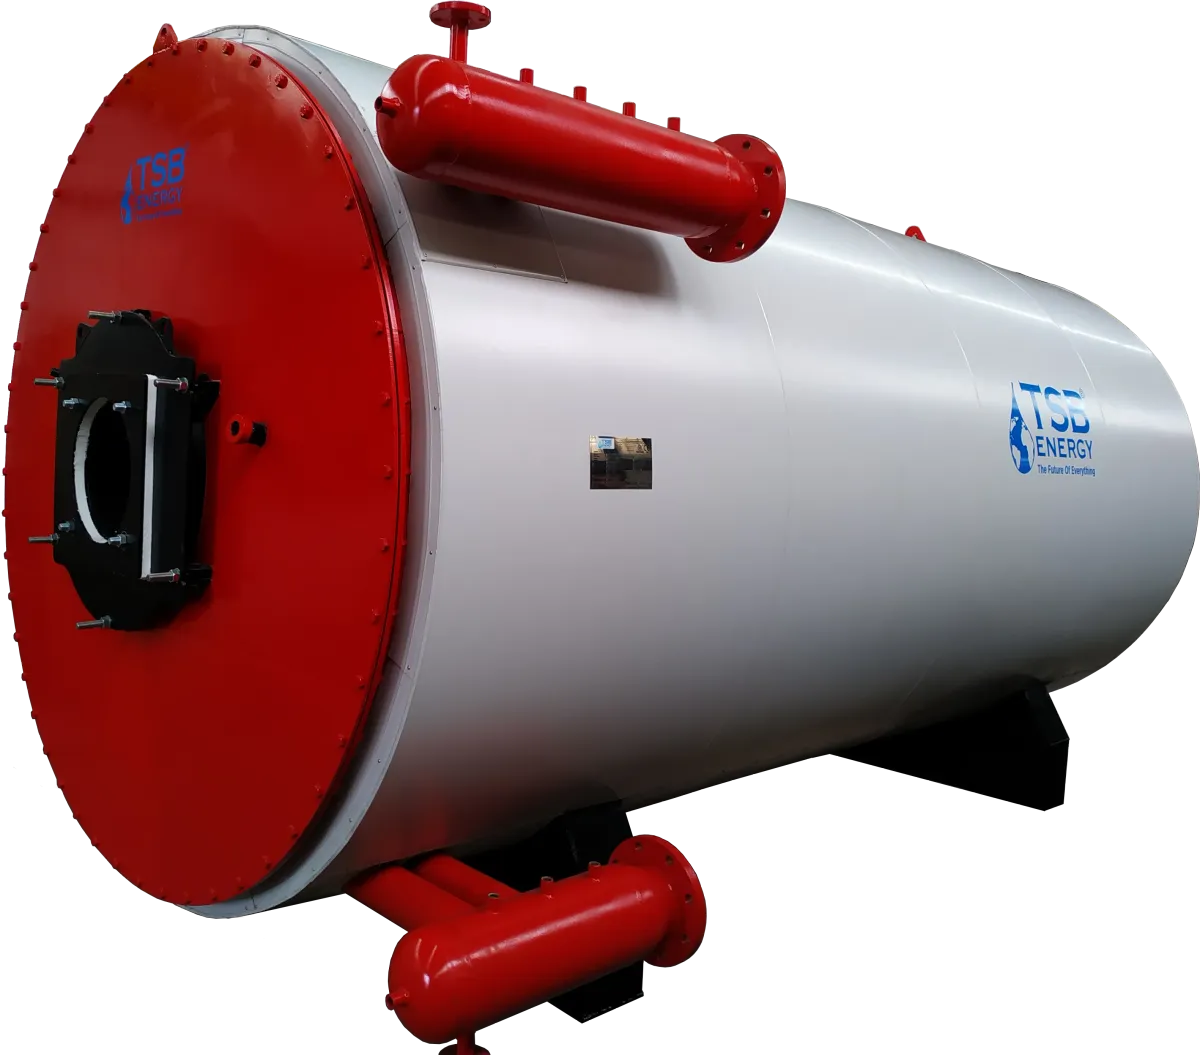
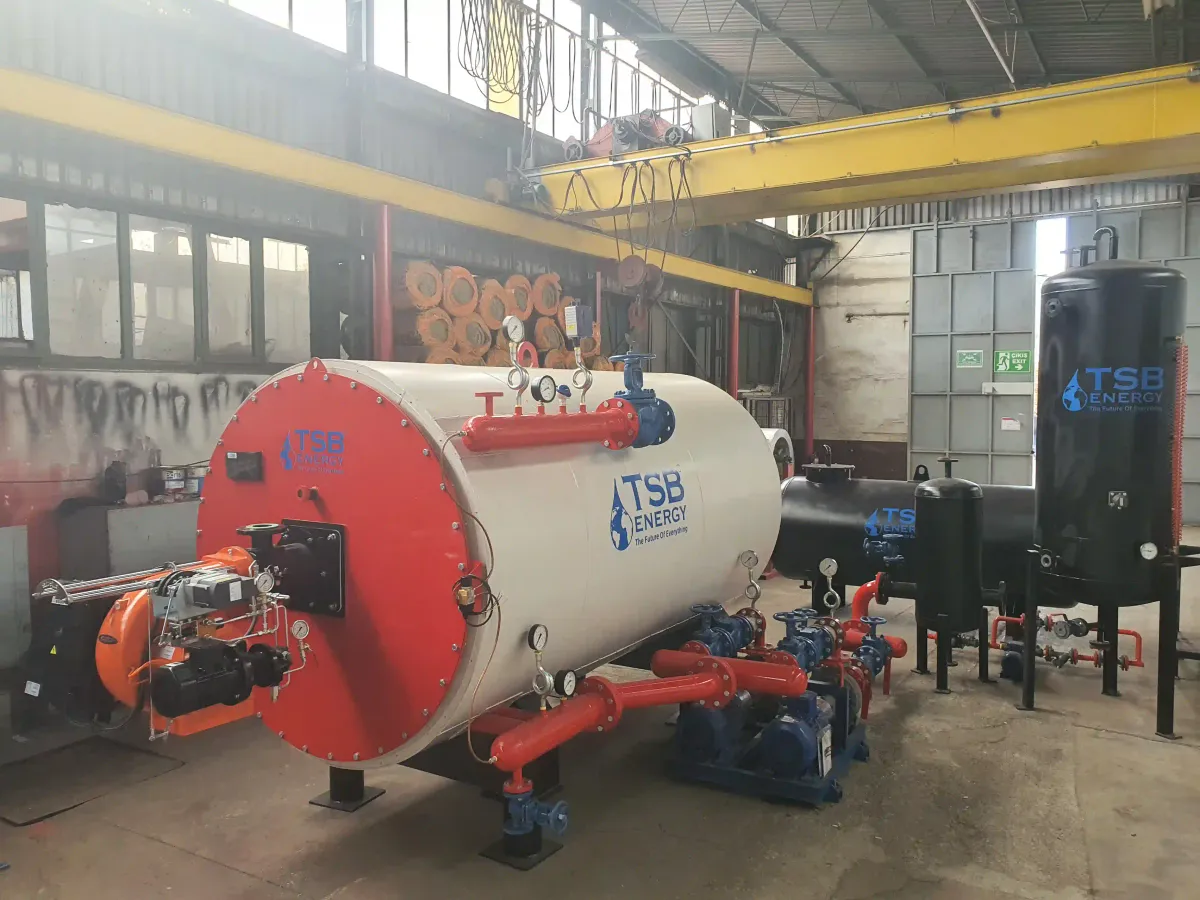
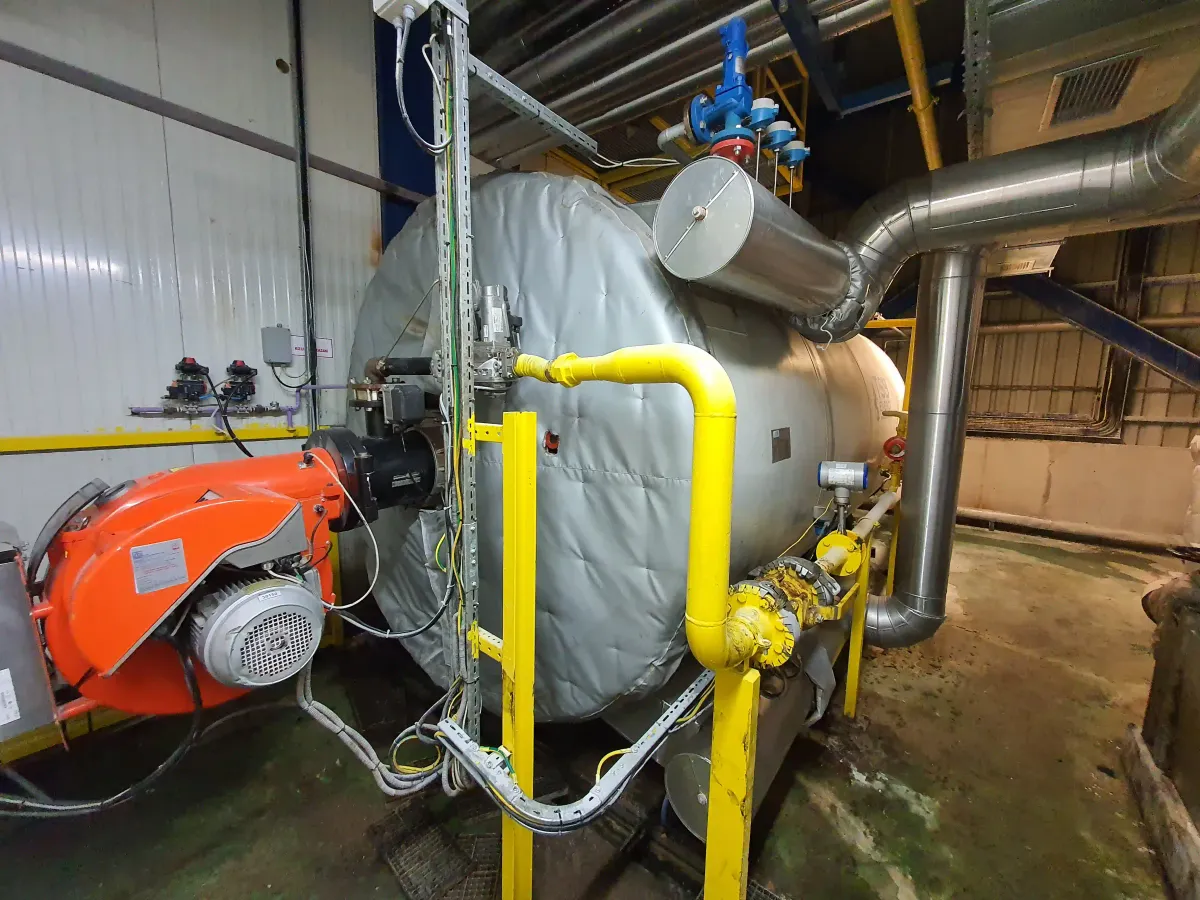
Liquid and gas-fired thermal oil heater
Forced-circulation coil heater that brings thermal oil up to 420 °C in a closed loop (special equipment above 300 °C)
TSB Energy
- ≤ 420 °C (special equipment > 300 °C)
- ≤ 12 000 kW
- ≤ 25 bar
The thermal oil heater is a forced-circulation heat transfer fluid heater in which a pump drives thermal oil through a series of coils. Special mineral or synthetic thermal oil flows through the coil tubes continuously at 1.5–2 m/s, turbulent and without dead spots, and is brought to the required temperature by the flame and flue gas in the combustion chamber. The pump is sized for the flow rate and pressure drop of each application, and combustion air and fuel are adjusted by PID control according to the oil outlet temperature. Thanks to the small volume and high flow velocity, the heater responds quickly to changes in load.
TSB Energy offers outputs up to 10 000 000 kcal/h (up to 12 000 kW) and pressures up to 25 bar; the oil temperature can be set up to 420 °C, with special equipment used above 300 °C. Fuels include natural gas, LPG, LNG, biogas, diesel and heavy fuel oil, plus up to 100 % hydrogen with a suitable burner. The heater is built in a horizontal or vertical layout, and its design follows DIN 4754, EN 13445, PED 2014/68/EU, TRD and ASME VIII Div. 1. Shell and covers are made of P355GH (EN 10028-2), boiler tubes of P235GH or P265GH (EN 10216-2).
Unlike steam, the fluid does not change phase: there are no steam traps, no flash steam or blowdown losses, no make-up water and no wastewater; water treatment and chemical conditioning are unnecessary, and under normal climatic conditions the installation does not freeze in winter. According to TSB, 20–40 % less energy is needed than with steam to transfer the same heat. A three-layer insulation on the front door and the reversal chamber cover — alumina-enriched refractory concrete, ceramic fibre blanket and ceramic paper — keeps the cover cool enough to touch.
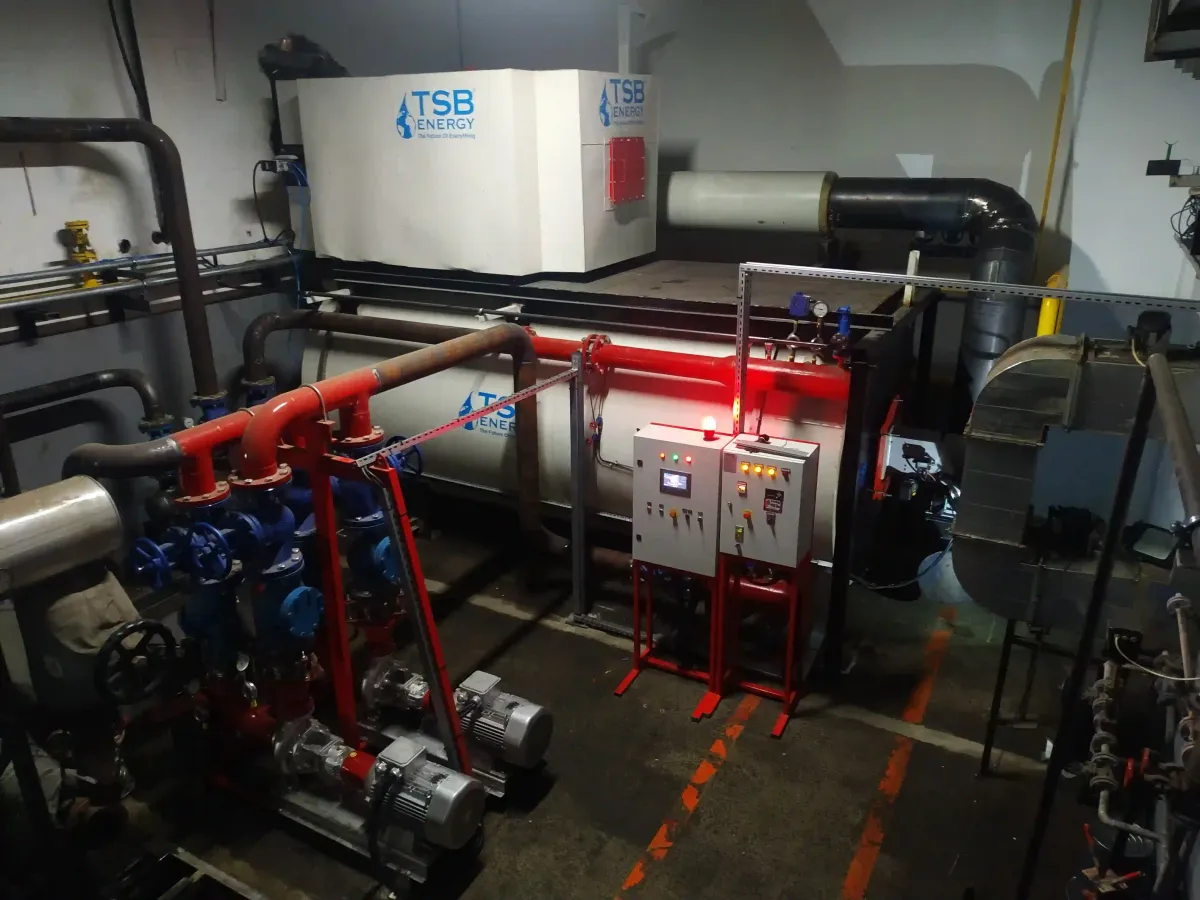
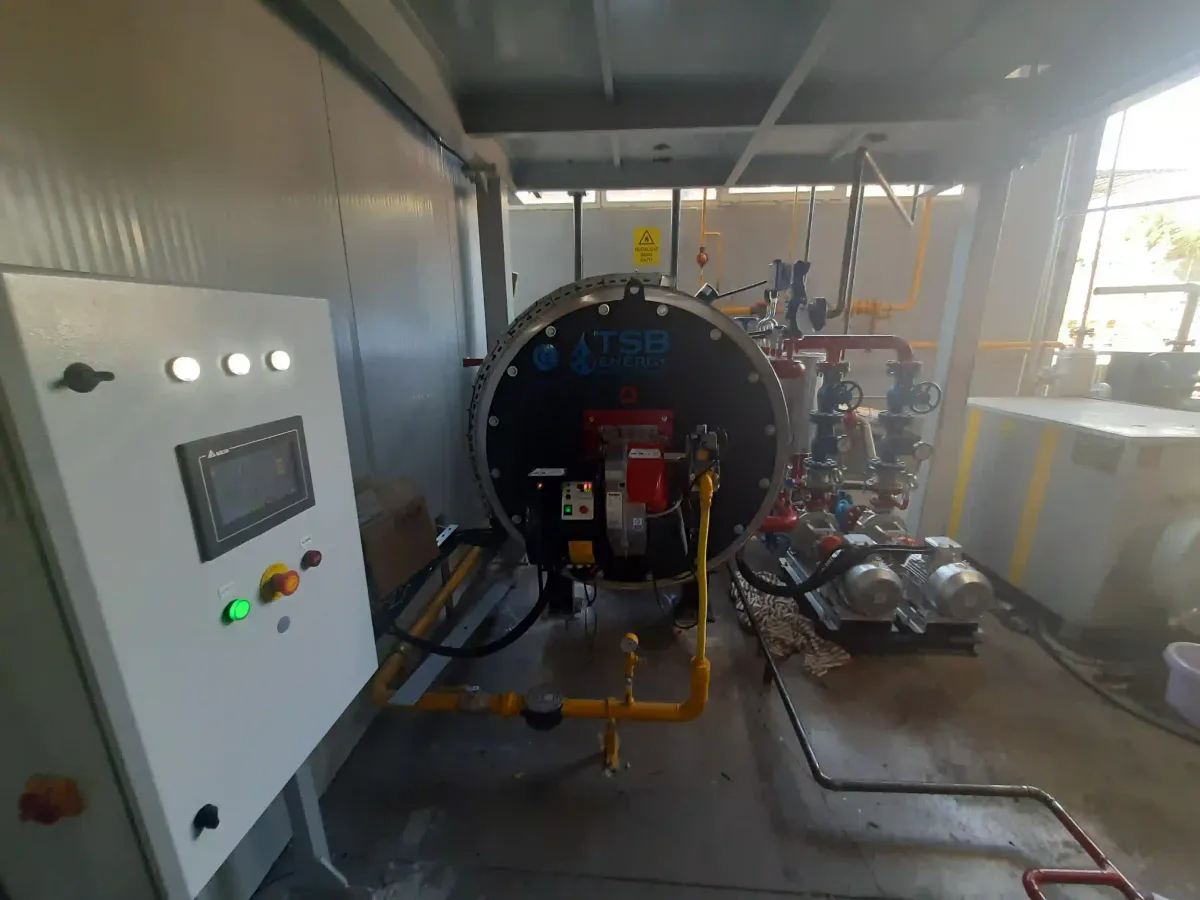
Liquid and gas-fired thermal oil heater
- No water treatment, conditioning or chemicals needed for the thermal oil
- Closed, loss-free circuit with no scale or corrosion problems
- Horizontal or vertical construction fits almost any site
- Precise, constant temperature control
- Flow monitoring built into the heater design on every unit
- Tube and coil diameters redesigned for low oil back-pressure, allowing lower-power electric motors
- Optional recuperator uses the flue gas to preheat combustion air for higher efficiency
- 24 to 720 hours of unattended operation lowers running costs
Key specifications
| Specification | Liquid-Gas Fired Thermal Oil Heater |
|---|---|
| Thermal capacity | ≤ 10 000 000 kcal/h (≤ 12 000 kW) |
| Operating pressure | ≤ 25 bar |
| Operating temperature | ≤ 420 °C (special equipment > 300 °C) |
| Flow velocity | 1.5–2 m/s (thermal oil in the coils) |
| Fuel types | Natural gas, LPG, LNG, biogas, diesel, heavy fuel oil, H₂ (up to 100 % with a suitable burner) |
| Unattended operation | 24–720 h |
| Design | Spiral coil bundle; horizontal or vertical |
| NOx emissions | Clean combustion: < 70 mg/Nm³ (gas firing) · < 150 mg/Nm³ (oil firing) |
| Material | Shell and covers: P355GH (EN 10028-2) · boiler tubes: P235GH / P265GH (EN 10216-2) |
Approvals and standards
- DIN 4754 — heat transfer oil systems (design and manufacture)
- EN 13445 — unfired pressure vessels (design and manufacture)
- PED 2014/68/EU — Pressure Equipment Directive (design and manufacture)
- TRD — German technical rules for steam boilers
- ASME VIII Div. 1 — pressure vessels (design and manufacture)
Accessories
- Expansion and reserve tanks with a system deaerator
- Pumps for circulating the thermal oil
- Valves and control equipment for the system
- Recuperator heating the combustion air with flue gas
- O₂ and CO trim control
- Firing options for two fuels or fuel mixtures
- PLC supporting communication protocols such as Modbus and Profibus
More products in this group
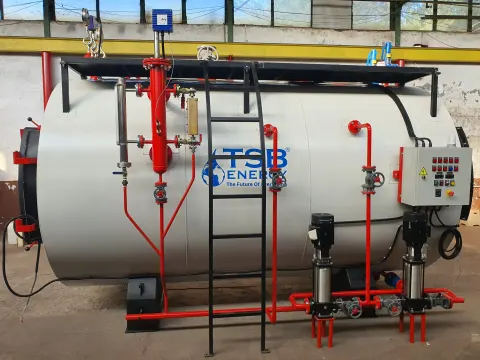
Three-pass steam boiler
Scotch-type fire-tube boiler for industry: up to 30 000 kg/h of steam at pressures up to 25 bar
- ≤ 30 000 kg/h
- ≤ 21 000 kW
- ≤ 25 bar
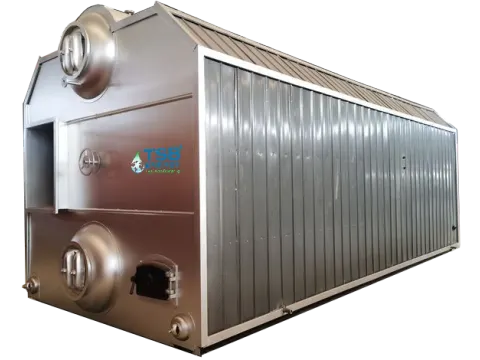
Water-tube steam boiler
Low-water-content boiler that raises steam in 10–15 minutes: up to 80 000 kg/h of steam at up to 160 bar
- ≤ 80 000 kg/h
- ≤ 160 bar
- Efficiency ≥ 95 %
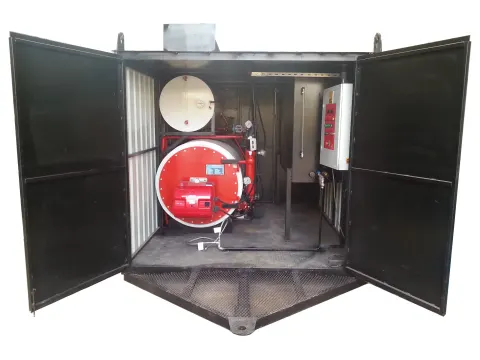
Mobile steam boiler room
Complete steam boiler house in a 20 ft or 40 ft ISO container, factory-tested and ready to connect
- ≤ 6000 kg/h
- ≤ 16 bar
- ISO 20 ft / 40 ft
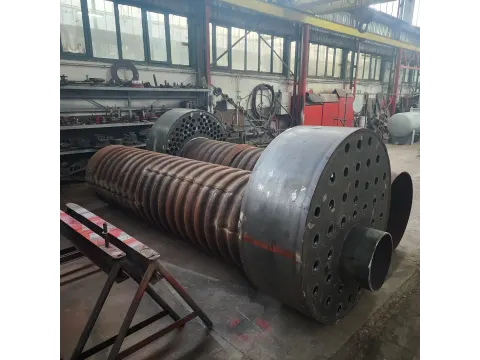
SWB superheated water boiler
Three-pass pressurised hot water boiler that keeps water liquid above its boiling point in a closed circuit
- ≤ 10 000 000 kcal/h
- ≤ 12 bar
- Efficiency 93–94 %
Let's choose the right product for your project together
Tell us about your plant and what you need, and our engineers will recommend the right solution.